How to Control Distortion in Thin Wall Aluminum Parts
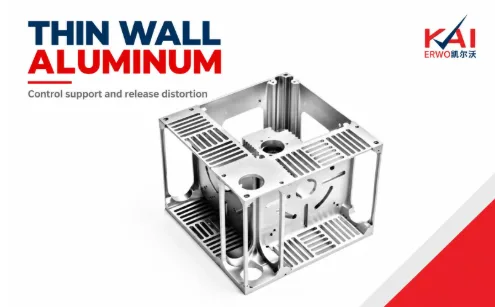
| Control thin wall distortion by first identifying when the movement occurs. A wall pushed away during cutting, a flange bent by clamping and a housing that moves after release require different corrective actions. The most useful evidence is a comparison of the same features during the route, after unclamping and under the defined inspection conditions. Wall thickness alone cannot predict whether a particular part will be stable.
For an aluminum cnc machining service, a useful DFM discussion should connect the wall geometry to its supports, stock condition and finishing sequence. Ask which material remains around the feature at each operation and how the delivered shape will be checked. A supplier’s ability to cut a small nominal thickness is not equivalent to a repeatable tolerance commitment on a tall unsupported wall. The following methods help turn a general concern about warping into a testable process investigation. Build a deformation map through the machining sequenceMeasure a thin component at meaningful stages rather than assigning one final error to a single cause. The blank condition, rough machined condition, clamped finish condition and released condition can reveal different mechanisms. Use the same reference features and a controlled measurement approach wherever possible. A change after release suggests a different investigation from an error that remains identical under all support conditions. Preserve the stage information even when the first trial fails; it can be more useful than a single final rejection measurement. Map where material remains during each operation. A wall supported by a thick floor during roughing may become flexible after that floor is reduced. A perimeter frame may stiffen a panel until the last cut separates it from the blank. The final model alone cannot show these changing support conditions. Review the operation sequence with intermediate shapes or marked views, especially around features that lose their support early. This helps identify whether a troublesome finishing pass could occur while more useful stiffness remains. Treat clamp location and force as separate variables. Moving a clamp toward a stiff region can change deformation even when the force is unchanged. Increasing force to prevent motion may create a larger released error. If a trial compares two fixtures, record contact points, support surfaces and the relevant tightening procedure so that the result can be interpreted. A fixture described only as more rigid does not explain how the part was constrained or whether it was being pulled into a different shape. Distinguish the acceptable product condition from the convenient measurement condition. A flexible cover may be intended to seat against a rigid frame, but that does not automatically permit arbitrary restraint during inspection. Define whether a free condition, an assembly condition or both are required. If assembly restraint is part of the acceptance method, state it clearly enough to reproduce. Otherwise, the supplier and customer can obtain different results without either instrument being faulty, simply because they measured different mechanical states. Distinguish elastic movement from permanent distortionA thin feature can move for several different reasons, and the remedy depends on the mechanism. Cutting force can elastically deflect a wall away from the tool; clamping can bend the entire component; residual stress can produce movement after material removal; and uneven temperature can change the measured shape. These effects may occur together. Before changing the program, compare the part during machining, after unclamping and after it reaches a stable temperature. Record the direction and location of the error rather than describing every problem as warping. Wall thickness alone is an incomplete feasibility measure. Height, unsupported span, neighboring ribs, base thickness and the direction of loading all affect stiffness. A short wall between heavy sections can behave very differently from a tall isolated fin of the same thickness. The remaining geometry also changes throughout the toolpath. Material that supports a feature during roughing may be removed before finishing, leaving the last pass in the least stable condition. Review the sequence as a series of changing structures rather than treating the finished solid model as the only stiffness model. Retaining temporary support can be useful. A sacrificial web, local tab or thicker section can carry cutting loads until nearby features are complete. Its removal must be planned: the final support cut can release stress or leave a difficult burr. Alternating material removal between opposite sides is another option when the geometry and access allow it. Sandvik Coromant identifies wall proportions and staged support as relevant to thin wall milling. [1] Its application guidance should be evaluated against the actual cutter, material and workholding, not copied as a universal design limit. Inspect thin parts in the condition relevant to their function. If a housing is bolted into a rigid assembly, the designer may need both a free condition requirement and an assembly verification. If the drawing requires free condition flatness, a fixture that pulls the part flat cannot establish compliance. State contact points, restraint and orientation where these affect the result. A light measurement force may also matter when a probe or indicator can displace the feature it is supposed to measure. A controlled trial changes one meaningful factor at a time. For example, compare clamping approaches while keeping the same stock and finish path, or compare roughing sequences while keeping the inspection condition fixed. Use the observations to decide whether the next change should target support, force, stock condition or temperature. Increasing material strength is not automatically a cure for an elastic stiffness problem. The useful outcome is a repeatable process and a defensible acceptance method, not simply one part that appears flat while it remains attached to the fixture. Compare the available choices
Make workholding part of the accuracy argumentA fixture must locate the part, resist the cutting loads and allow the required surfaces to be reached. These functions should be evaluated separately. Increasing clamp force can prevent slip while simultaneously distorting a thin component. Adding another support can reduce bending but overconstrain an irregular blank. Begin with a clear locating scheme, then place support and clamping forces where the part has sufficient stiffness. The important question is not how firmly the workpiece feels attached, but whether it occupies a repeatable position without unacceptable deformation. Check what happens when the part transfers between operations. A datum machined in the first setup can provide a better reference for the second than an unmachined stock face, but it must remain accessible and free from burrs. Soft jaws should contact the intended surfaces rather than accidentally seating on a radius or leftover stock. A chip beneath a locating face can alter angular alignment as well as height. Make cleaning and seating checks explicit steps in the process, especially when small position errors are amplified across a long part. Thin flanges and rings deserve a release check. A part can meet its apparent size while clamped and spring to a different shape after removal. Conversely, measuring a flexible part without a defined support condition can produce inconsistent readings even when its assembly behavior is acceptable. Agree the inspection state with the designer. If a restraining fixture represents the real assembly, document its contact locations and loading conditions. Do not quietly use the machining fixture to force a free condition requirement into compliance. Workholding cost should be compared over the intended production horizon. A simple vise may suit a few pieces but require several setups and repeated indicating. A dedicated fixture may reduce handling and improve access, although it introduces design effort, fabrication, maintenance and storage. Include spare locating elements and a method for checking fixture wear if the program will repeat. A fixture that works on one machine is not automatically qualified on another, particularly when the new machine changes access, load direction or available travel. Before production, ask for an operation sketch showing locating faces, clamps, supports and the features produced in that setup. This makes the supplier’s accuracy argument reviewable without requiring disclosure of every proprietary programming detail. If a critical feature is completed after several transfers, request an explanation of how its datum relationship is preserved. Verification should follow the same functional logic as the drawing, while retaining sufficient independence to detect an error introduced by the fixture itself. A hypothetical pocketed electronics housingConsider a hypothetical rectangular electronics housing with a thin floor and a mounting flange around its opening. The assumed requirement is that the flange seats on a rigid cover without excessive gap. The first trial looks satisfactory in the fixture but opens at one corner after release. This observation suggests that the fixture condition and the free condition need to be compared before changing a finishing offset. The team measures the flange with the drawing’s agreed support arrangement and checks whether clamp loading pulls it into a different shape. It also compares measurements after roughing and after the final pocket pass. If the shape changes after bulk removal even with restrained clamp loads, stock condition and sequencing become stronger candidates. If the difference mainly follows clamp force, workholding deserves priority. Neither conclusion should be made from a single unrepeatable reading. A revised route is then tested using the same inspection conditions. It may retain support material longer or change how the flange is held, depending on the evidence. The team accepts the change only if the released geometry and the relevant surfaces improve together. This is a hypothetical diagnostic example, not a reported production result or a guarantee that one specific fixture strategy will work for every housing. Diagnose vibration by its pattern and its supporting conditionsA repeated pattern on a machined surface is evidence to investigate, not a complete diagnosis. Vibration may involve the cutter, holder, spindle, fixture or workpiece, and more than one element can be flexible. Record where the marks occur, their direction, the operation and whether the sound or surface changes with depth. Compare straight cuts with corners and heavy engagement with light finishing. This helps identify whether the problem follows the tool assembly, the local part stiffness or a particular change in cutting conditions. Start with basic mechanical checks. Verify tool seating, runout, holder condition, clamping contact and the absence of trapped chips. Confirm that the actual overhang matches the planned setup. A tool extended further than expected can behave differently even when the program and material are unchanged. Review whether the remaining workpiece still has the support assumed during programming. Sandvik Coromant’s vibration guidance treats the complete machining system as relevant. [2] It does not justify assuming that every visible mark can be cured by one spindle speed adjustment. Use parameter trials carefully. Changing speed can alter the dynamic response, while changing feed or engagement affects chip formation and force. Lowering every value at once makes it difficult to learn which mechanism mattered. Excessively light cutting can introduce rubbing, and a slower process can still leave the same defect. Choose a plausible change, define what improvement should be observed and inspect the result under the same conditions. Retain successful settings with their tool assembly and workholding context so that they remain reproducible. Distinguish surface appearance from dimensional performance. A quieter cut may still leave a tapered wall because the tool deflects steadily. A visually improved surface may not satisfy the specified texture when measured. Conversely, a cosmetic mark outside the functional region may not justify an expensive redesign. Check the actual acceptance requirements and determine which failure is limiting the part. If the same operation must control both geometry and texture, the trial should measure both rather than optimizing one at the expense of the other. Escalate to a structural or process change when adjustments do not create a stable window. Options can include a shorter tool, a different holder, added support, a revised sequence or a different approach direction. A designer may be able to enlarge a nonfunctional opening or retain a rib that improves stiffness. Evaluate the consequences of those changes on the complete assembly. The final process should have enough margin to survive normal variation in stock, tool condition and setup, not merely produce one attractive surface during a carefully managed demonstration. Use controlled trials to select a practical correctionBegin a correction trial with a hypothesis that can be disproved. If the wall is deflecting under cutting load, a change in support or engagement should alter the observed pattern in a physically consistent way. If residual stress dominates, a revised stock condition or removal sequence may matter more than the last finishing pass. If the apparent error is thermal, stabilizing measurement conditions should change the conclusion. Changing all three at once may produce a better part but leave the process poorly understood. Choose the trial response before machining. For a wall problem, the useful evidence may include thickness at several positions, released flatness and the direction of displacement relative to the tool path. A photograph of a smoother surface does not establish that dimensional deformation improved. Keep the measurement method unchanged unless the method itself is under investigation. If a different instrument is necessary, establish how its result relates to the previous evidence before interpreting the apparent improvement as a process effect. Consider redesign when the route becomes fragile. Adding a rib, reducing unsupported height or changing a pocket boundary may improve the structural condition, but each proposal needs an assembly and load review. Temporary tabs can support manufacture without changing the final geometry, yet their removal can create a new deformation event. Compare the complete routes, including support removal, edge finishing and inspection. A correction is incomplete if it merely moves the problem to the last operation. Define what will be monitored after the trial. A process that succeeds with one unusually favorable blank may remain sensitive to stock variation. A fixture that works only when adjusted by one operator may need clearer setup controls. Record the selected stock condition, critical support method, process sequence and acceptance state. The aim is not to promise zero distortion; it is to keep distortion within the required limits and to detect conditions that threaten those limits before the affected parts reach assembly. Account for thermal behavior before adjusting the tool offsetA metal component and its measuring equipment can change dimension with temperature. If the part is measured immediately after machining, handling or washing, the result may not represent its stable condition. Temperature gradients can also change shape rather than merely scaling every dimension uniformly. Begin by recording where and when measurements are made, how parts are handled and whether they have reached an appropriate thermal condition. A fixed waiting period copied from another job is less useful than evidence that the relevant part and instrument have stabilized. For a simple uniformly heated length, the first order model is change in length equals expansion coefficient multiplied by original length and temperature change. As a hypothetical calculation, assume a coefficient of 23 micrometers per meter per kelvin, a length of 100 mm and a uniform increase of 5 K. The predicted change is 11.5 micrometers. The coefficient is an explicit illustrative assumption; use the supplied alloy and temperature range data for a real calculation. A hollow housing with uneven heating can require a more detailed analysis than this one dimensional model. Measurement compensation requires reliable inputs. An assumed material coefficient, a temperature sensor far from the critical feature or a tool that has not stabilized can undermine the correction. The measuring system and the part may have different thermal behavior. Document whether the result is a raw reading or a compensated value, and use the drawing’s agreed reference conditions. Do not apply multiple independent corrections without understanding whether the instrument software already accounts for the effect. Thermal effects can appear as production drift. A machine warming from a cold start, changing coolant conditions or a different pattern of heavy cutting can alter the dimensional trend. Record the sequence of parts and the timing of measurements before changing offsets. If an adjustment is based on a temporarily warm part, the process may later move away from target when the thermal condition changes. Comparing stabilized measurements with in process observations helps distinguish actual cutting variation from changes in the measurement state. Consider service temperature separately from inspection temperature. A mating aluminum housing and steel insert can experience a different change in clearance as the assembly heats. A fit that is acceptable on the inspection bench may bind or loosen in operation. Include the operating range, constraints and material combination in the interface calculation. This does not justify changing drawing limits informally; it provides the engineering basis for selecting them. Manufacturing, inspection and service conditions should form one consistent dimensional argument instead of three unrelated assumptions. Separate material removal from the final definition of the partA machining sequence should preserve access, support and references until they are no longer needed. Roughing removes the bulk of the stock; finishing establishes the surfaces that will be accepted. These stages need not occur in a single uninterrupted setup. For a heavily pocketed component, it can be useful to leave controlled material on important surfaces, release or reposition the part, and finish only after the effect of bulk removal is understood. The appropriate sequence depends on stock condition and geometry, not on a universal rule that more operations are always better. Plan datums before planning individual dimensions. Establish a stable reference surface early enough that later features can be related to it, but avoid finishing it so early that subsequent clamping damages it. If the final datum is a thin face created near the end, use temporary manufacturing references and explain their relationship to the final inspection system. The programmer’s convenient coordinate origin and the drawing’s functional datum reference frame serve different purposes. A good process connects them deliberately instead of assuming they are automatically the same. Hole and edge operations also interact. Drilling into an already finished pocket can create an inaccessible burr at breakthrough. Machining the intersecting cavity later may remove that burr, but can also damage a finished bore edge. Threading before an aggressive surface treatment may require allowance or masking; threading after treatment can leave exposed material. Map these interactions on a simple operation list. Identify where inspection, cleaning and deburring must occur before a feature becomes difficult to reach. Do not treat an extra finish pass as a guaranteed correction. If the part moves away from the tool during the first pass, a second pass may remove additional material, but it can also rub without producing a stable chip. If the underlying problem is a moving fixture or changing temperature, repeating the same path can conceal rather than eliminate the cause. Determine whether the remaining stock and tool engagement justify the planned finishing operation. A process should have a defined acceptance check, not an indefinite cycle of recutting until one measurement looks right. The sequence should end with verification of the delivered condition. Include outside coating, heat treatment, cleaning or marking when these can affect dimensions or surfaces. A dimensional report completed before an operation that changes the interface may be useful process evidence but incomplete delivery evidence. Ask which characteristics are rechecked after the last relevant operation and how parts are protected afterward. This closes the gap between a successful machining operation and a finished component that will actually assemble and function as intended. A practical review sequence1. Record the error location and compare restrained, released and thermally stable measurements. 2. Examine the changing support geometry throughout roughing and finishing. 3. Test one plausible cause using consistent stock and inspection conditions. 4. Verify the released part and the assembled interface before approving the revised route. Common mistakes and better decisionsAdding clamp force can make a part appear more stable while increasing release distortion. Another mistake is reducing feed repeatedly without checking whether the cutter is rubbing or the wall has lost support. A stronger alloy can also fail to solve an elastic flexibility problem. Diagnose the mechanism, then change the relevant support, sequence, material condition or cutting strategy and measure the result. Frequently asked questionsIs there a universal minimum aluminum wall thickness?No. Height, span, support, tool access, alloy condition and the acceptance limits all matter. A supplier should assess the actual feature. A successful demonstration on a short rib does not prove capability on a large unsupported housing wall. Should flatness be checked while the part is clamped?Use the condition specified for acceptance. If free condition flatness is required, a fixture that forces the part flat cannot prove compliance. If an assembly restraint is relevant, define it explicitly and keep it distinct from the machining clamp condition. Will an extra finishing pass remove distortion?It may help a particular cutting deflection problem, but it is not a universal remedy. It can also rub or remove material from a part that later moves again. Check the source of movement and the remaining stock before adding repeated passes. Can a temporary web be left in the design?It can be a manufacturing aid if its removal is planned and the final part remains compliant. Review the last cut, resulting burr and release movement. Temporary support should have a defined removal and inspection step rather than an informal shop floor instruction. What should a thin wall prototype test demonstrate?It should demonstrate the required final shape, usable surfaces and intended assembly behavior under stated conditions. If production repeatability is the next decision, include multiple representative setups or events. One carefully handled sample provides limited evidence about a later batch. Prepare the next technical discussionSend the housing model, material condition, wall geometry, mounting interfaces, quantity and required free or restrained inspection state. For CNC prototyping services, request a DFM review that explains support and release checks, together with a quotation for the agreed final geometry. References[1] Sandvik Coromant. Shoulder milling. Online application guide, undated; accessed 22 September 2026. [2] Sandvik Coromant. How to reduce vibration in milling. Online application guide, undated; accessed 22 September 2026. |
||||||||||||||||